Hot Rolled Steel Framing Specification: Sections, Grades and Mill Documentation

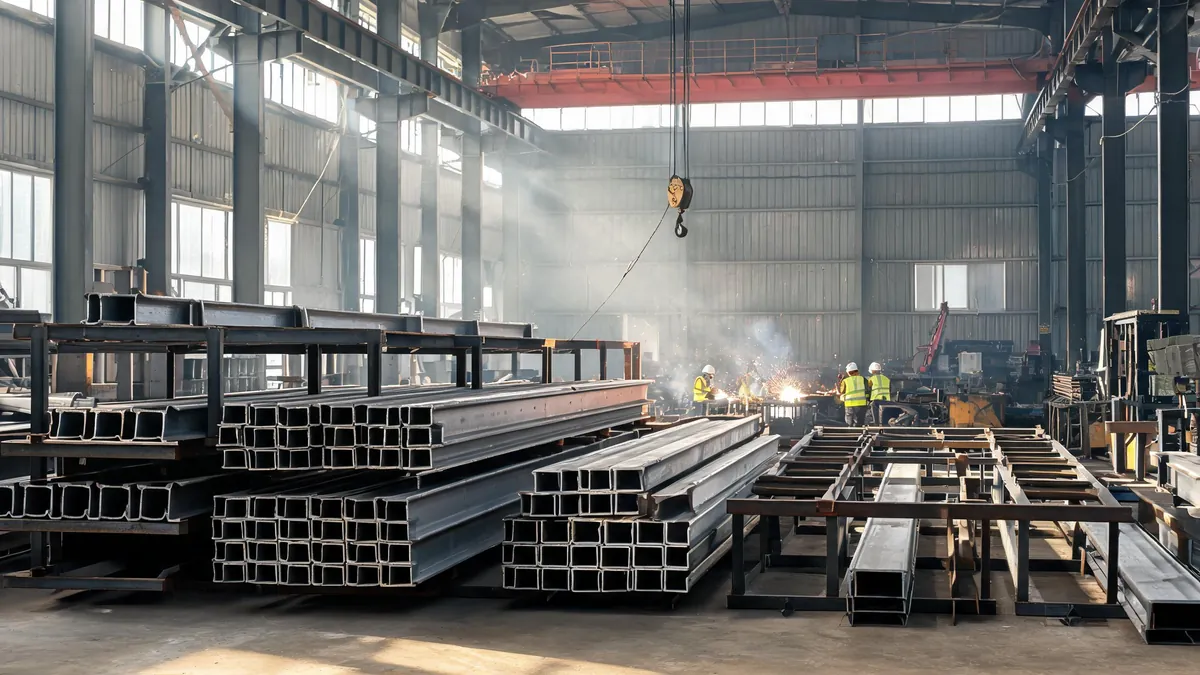
Hot rolled steel framing is the load-bearing skeleton of a warehouse package: the columns, rafters and crane beams rolled to a fixed section profile at a mill, rather than folded from thin coil. When a supplier quotes “steel structure”, the number that decides how your building behaves is not the total tonnage. It is the section family, the steel grade and the mill documentation sitting behind that tonnage. A 5% saving on tonnage achieved by swapping HN beams for a lighter profile, or by accepting a certificate that cannot be traced back to the member in the bundle, is a decision that shows up months later during erection or during an approval review.
This guide follows the order a design office and a fabricator actually work in: what hot rolled framing covers in a package, which section families appear in real quotations, how grades and certificates are verified, how surface preparation and tolerances follow from the section choice, and what to ask a fabricator before you place a purchase order. If you are still deciding whether the building should use hot rolled or cold formed members at all, start with our comparison of cold formed and hot rolled framing and then come back to specification detail here.
What hot rolled steel framing covers in a warehouse package
Hot rolled sections carry the primary loads. Everything else in the package — purlins, girts, roof sheets, wall panels, doors — hangs off them or transfers load into them. That hierarchy matters when you review a quotation, because a supplier can legitimately reduce plate weight in the secondary members and still describe the building as “hot rolled steel framing”.
| Package item | Usual material form | Hot rolled? | Typical specifier |
|---|---|---|---|
| Columns and rafters (portal frame) | Hot rolled H/I sections, or welded built-up H sections for long spans | Yes | Structural designer |
| Crane runway beams | Hot rolled I/H sections, or plate girders on heavy duty | Yes | Structural designer with crane supplier input |
| Splices, haunches, stiffeners | Hot rolled plate | Plate, not section | Fabricator detailer, approved by designer |
| Purlins and side girts | Cold formed C or Z sections; hot rolled angles in heavy roof zones | Usually cold formed | Designer / supplier standard system |
| Roof and wall bracing | Hot rolled angles, CHS or RHS | Yes | Structural designer |
| End plates, base plates, gussets | Hot rolled plate | Plate, not section | Fabricator detailer |
| Anchor bolts and cast-in items | Reinforcing steel and forged rods | No | Foundation designer |
Two practical consequences. First, when someone says “the frame is hot rolled”, confirm whether that includes the crane beam and the braces — those are the items most often quietly changed to welded plate or cold formed. Second, ask what is excluded: plates, bolts, anchor bolts, purlin laps and roof sheets are separate line items in a good quote, and a cheap quote often looks cheap because they were assumed, not designed.
Section families you will actually see in quotations
Hot rolled framing is not one product. The designation tells you the shape logic, and the shape logic tells you how the fabricator will cut, fit and weld it.
| Family group | Examples | Shape character | Where it lands in a portal frame | Fabrication note |
|---|---|---|---|---|
| Narrow flange H | HN series (GB/T 11263), some IPE sizes | Narrow flange, thinner web | Rafters and beams where bending governs and shear is modest | Lighter to handle; watch web panel zone when concentrated loads appear |
| Medium flange H | HM series | Middle web and flange thickness | Columns in mid-span frames, transfer members | Good compromise when spans are long and forces grow |
| Wide flange H | HW series, HEA/HEB, W shapes | Wide flange, thicker web | Columns, crane columns, heavily loaded rafter ends | More welding for stiffeners and base plates; heavier erection pieces |
| Universal I beams | IPE, some regional I sections | Slender, parallel flange | Secondary framing, runway support, tie beams | Cheap per metre, limited when spans exceed what the section depth allows |
| Hollow sections | CHS, SHS, RHS | Closed profile | Bracing, truss chords in some packages, columns in special designs | Closed ends need sealing and coating attention; connection detail is more demanding |
| Welded built-up H | Fabricated from plate | Any depth and taper the project needs | Long span rafters, tapered haunches, very heavy crane columns | Adds welding, distortion control, NDT and dimensional measurement to the scope |
Why the section family changes fabrication hours
The mill rolls a standard profile; the fabricator then fits plates, drills holes and welds. A wide flange column with a thick web needs more heat input and more distortion control than a thin web rafter of the same length. A tapered built-up rafter needs plate cutting, fit-up jigs and weld sequence control. None of that appears in a per-tonne rate comparison unless you ask for it.
Where spans grow beyond what a rolled section covers economically — commonly somewhere in the region of 35 m to 45 m for a single clear span portal, depending on loading, code and section availability — designers usually move to a heavier rolled section, a tapered built-up rafter, or a different structural system altogether such as a truss. The break point depends on your loads, not on a rule of thumb, so treat it as a design question rather than a purchasing preference.
Steel grades: what a designation actually promises
Grade selection is where procurement teams get caught, because the same nominal strength can come with very different toughness, chemistry and weldability. The table below is a map of common designations, not a substitution table.
| Designation | Standard | Nominal minimum yield (MPa, typical) | Where it is used | What to confirm |
|---|---|---|---|---|
| Q235B | GB/T 700 | 235 | Secondary framing, moderate spans, general structures | Impact requirements by thickness; project specification may demand higher |
| Q355B | GB/T 1591 | 355 | Primary members in Chinese-designed packages | Chemistry and carbon equivalent for weldability |
| S235JR / S355JR | EN 10025 | 235 / 355 | European-specified projects | Toughness class: JR loses impact properties below certain temperatures, J0/K2 do not |
| A36 | ASTM A36 | 250 | US-specified general structures | Older projects often upgrade primary members |
| A572 Gr 50 | ASTM A572 | 345 | US-specified primary framing | Strength matches Q355B closely; acceptance is a code question, not a chemistry question |
| A992 | ASTM A992 | 345 | US wide flange shapes | Shape availability outside the US |
| AS/NZS 300 / 350 | AS/NZS 3679 | 300 / 350 | Australia and New Zealand projects | Certified rolling availability and marking requirements |
Substitution is not automatic, even when the numbers look close
A 355 MPa designation and a 345 MPa designation sit next to each other on paper. The accepting engineer still has to confirm three things before a substitution note is issued: that the design code allows the substitute, that the toughness class suits the lowest service temperature on site, and that the chemistry is compatible with the welding procedure the fabricator intends to use. Low temperature toughness is the one that catches people out — a JR-class section on a cold-climate site is a durability risk regardless of strength.
Practically, the substitution process should run before cutting starts. If the fabricator finds that a section is unavailable after the material has been cut, the options are re-certification of the affected members at cost and delay, or remedial design. Both are avoidable with a two-line substitution clause in the purchase order and a material list reviewed against mill availability at the drawing approval stage. Our notes on steel grades Q235B, Q355B and S355 cover the practical side of that review.
Short answer to a question we get every month: can Q355B be substituted for A572 Grade 50? Mechanically the two are close, and in many exported packages they are treated as interchangeable in strength terms. The decision is still made by the engineer of record for the project, and it depends on the design code, the toughness requirement and local acceptance practice. Get it in writing before fabrication, not after.
Mill certificates, heat numbers and traceability
A mill test certificate is only useful if you can connect it to the steel you received. The connection is the heat number, and the heat number only survives if the fabricator’s marking system carries it through cutting, welding and packing.
| Document | Issued by | What you check | Common gap |
|---|---|---|---|
| Mill test certificate (EN 10204 3.1 or equivalent) | Steel mill | Heat number, standard, chemistry, mechanical properties, dimensions, quantity | Certificate supplied for a heat, but no link to which members used it |
| Material purchase records | Fabricator | Mill name, heat numbers, purchase dates, quantities | Third-party supplied steel with certificates from a trader rather than the mill |
| Shop drawings | Fabricator detailer | Section sizes, grades, splice and hole positions, member marks | Member marks on drawings that do not match marks on the bundle tags |
| Dimensional inspection report | Fabricator QC / third party | Lengths, straightness, hole positions, base plate flatness | Report covers a sample lot rather than the shipped lot |
| Welding documentation | Fabricator QC | WPS/WPQR references, welder IDs, NDT results for defined joints | NDT scope described as “as required” with no agreed percentage |
| Packing list | Fabricator | Member marks per bundle, weights, container allocation | Marks not readable after packing, forcing site sorting |
The cheapest control point is an agreed marking scheme. One heat number per member is impractical on a large job, but a rule such as “each member carries the frame mark; each bundle tag carries frame mark, section size, grade and heat number range” gives you a traceable path from certificate to installed steel without slowing the line. Put that rule in the purchase order and check it during the pre-shipment inspection, not at the port.
Do you need third-party inspection for hot rolled framing? Not always, but define the witness points either way. A workable scope for an export warehouse package is: material certificate review and marking check before cutting, dimensional check on completed frames, NDT on full-penetration welds at a stated percentage, coating thickness and adhesion checks, and a pre-shipment bundle count against the packing list. If you are buying through a trading company rather than the fabricator, add a clause that lets you verify the actual production site. We describe the evidence set in more detail in our note on weld quality and NDT evidence.
Reconciling the take-off: the tonnage you are paying for
Most buyers compare quotations on price per tonne. The problem is that two quotations rarely describe the same tonne. Plates, bolts, purlins and connection material are sometimes inside the weight and sometimes excluded, and the allowance for splices and stiffeners varies from fabricator to fabricator.
You do not need a full take-off to sanity check a quotation. You need a section list, and then four questions:
- Which members are priced by section weight, and which are priced as plates?
- Is the quoted tonnage the finished painted weight, the bare steel weight, or an estimate rounded up?
- What percentage is allowed for connections, stiffeners, haunches and base plates — and is that allowance stated or hidden?
- Does the tonnage match the drawing revision you approved?
A useful discipline is to ask for the take-off as a table: member mark, section size, grade, length, quantity, unit weight, total weight. Some fabricators will not release their full take-off commercially, but every fabricator can release the summary by section size. That summary lets you check the structure of the quote, and it becomes the baseline for any variation later.
| Design decision | Effect on tonnage | Effect on fabrication hours | Watch out for |
|---|---|---|---|
| Longer clear span for the same area | Rises — deeper sections and heavier rafters | Rises, and handling becomes harder | Foundation loads grow faster than the steel weight |
| Wider bay spacing | Falls slightly on primary steel, rises on purlins | Falls on primary, rises on secondary | Purlin and cladding spans must still be checked |
| Higher eave height | Rises — taller columns and more bracing | Broadly unchanged per tonne | Bracing layout becomes the governing item |
| Crane loading added | Rises sharply on columns and runway beams | Rises — fatigue details, NDT, tighter tolerances | Runway beam alignment tolerances drive site cost |
| Heavier roof build-up (insulation, solar, suspended services) | Rises | Broadly unchanged | Loads must be in the design basis, not assumed later |
| Substituting a heavier grade | Falls slightly — smaller sections for the same capacity | Broadly unchanged | Stiffness, not just strength, may govern deflection |
| Hot dip galvanizing instead of paint | Unchanged | Rises — handling, venting and drainage details | Closed sections and overlapping plates need vent holes |
Surface preparation, coatings and what the hot rolled surface does to them
Hot rolled steel arrives with mill scale, and mill scale behaves differently from bare steel under a coating. It is hard and dense; it also flakes, and a coating applied over a loosely adhered scale layer will fail with it. That is why coating system selection starts with surface preparation, not with the paint brand.
| Exposure context | Typical preparation | Typical protection | Inspection point before shipment |
|---|---|---|---|
| Dry inland, covered by cladding | Manual or power tool cleaning to remove loose scale and rust | Shop primer or one-coat system | Coverage on edges, cut ends and weld zones |
| Humid or coastal atmosphere | Abrasive blast to a defined cleanliness grade | Multi-coat paint system with total dry film thickness specified | Blast profile, inter-coat times, DFT readings |
| Aggressive coastal or chemical exposure | Abrasive blast to a higher cleanliness grade | Hot dip galvanizing to a defined standard, sometimes duplex with paint | Coating thickness, drain and vent holes, thread protection |
| Mixed: galvanized frame, painted plates | Depends on the item | Combination systems | Compatibility of paint on galvanizing — passivation and primer choice |
Two details get missed on hot rolled framing specifically. First, cut ends and weld areas have no mill scale and no factory coating, so they corrode first; the specification should say what happens at cut edges and welds. Second, galvanizing a frame assembled with overlapping plates can trap liquid and cause distortion unless vent and drain holes are detailed on the shop drawings. Both are drawing-stage decisions with a cost consequence if they are fixed later.
Fabrication tolerances and connections that follow from the section choice
Tolerances are where a warehouse package succeeds or fails during erection. The frame is not a machined product; it is a welded assembly, and the permitted deviation has to be defined in a way the fabricator, the inspector and the site crew all read the same way.
For each shipment, agree three numbers: member length tolerance, hole position tolerance, and frame squareness or diagonal tolerance. Then agree how they will be measured and reported. A dimensional inspection report that lists only “within tolerance” without the measured values gives you nothing to work with if a portal does not line up on site.
Connection details that get decided late
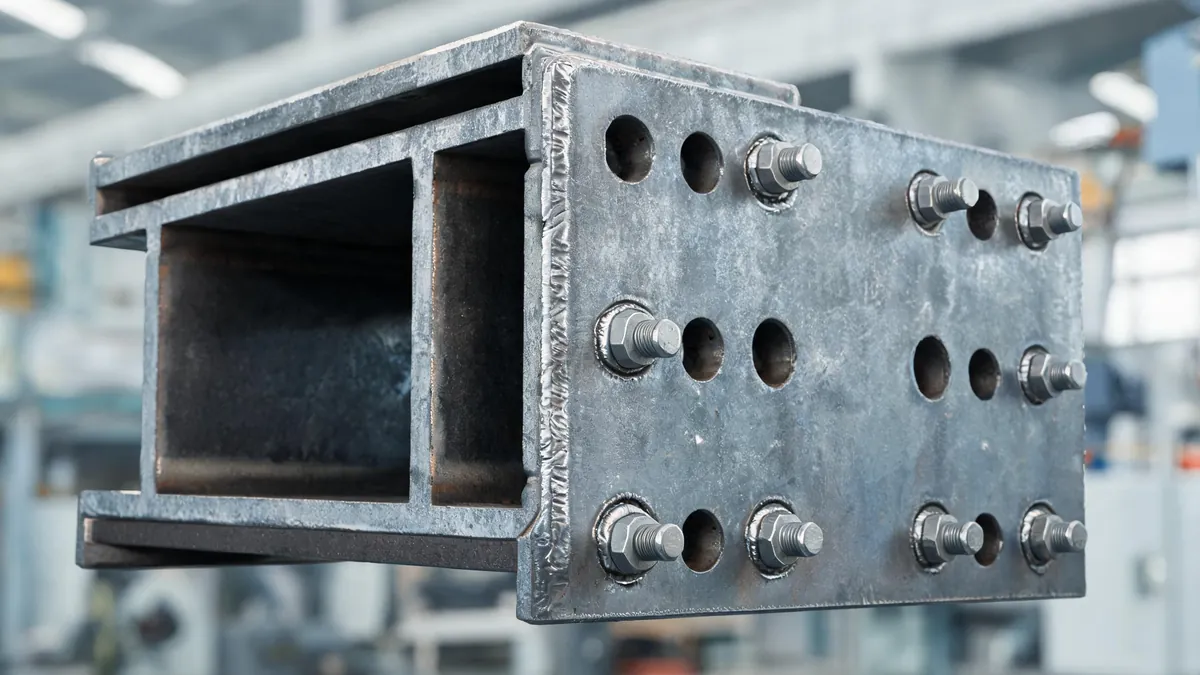
- Splice positions. Where the rafter or column is spliced determines whether the splice sits in a low-moment zone and whether it can be shipped and lifted. Moving a splice later changes plates, bolts and painting.
- Haunches. A haunch adds steel near the eaves, where bending is highest. Its shape and welding access decide the fabrication hours for that connection.
- Stiffeners and web panels. Concentrated loads at crane brackets or heavy purlin connections usually need stiffeners. If they are not on the drawing, they appear as a variation.
- Base plate and anchor bolt interface. The hole pattern on the base plate and the setting out of the anchor bolts must come from the same drawing revision. This is the single most common source of site grinding; our note on anchor bolt and foundation data covers what the fabricator should hand over.
- Bolt grade and pretensioning. Ordinary bolted connections and pretensioned friction connections have different bolt grades, surface conditions and inspection requirements. State which applies.
Where hot rolled framing stops being the economical answer
Three honest limits. When the span exceeds what a rolled section can serve efficiently, welded built-up members bring extra fabrication and NDT. When the building is small and lightly loaded, a cold formed system can be cheaper and faster — the trade-off is different detailing and different site skills. And when shipping volume, not weight, is the constraint, lighter sections do not help because the container is already full. Identifying these limits early avoids designing a frame that is technically correct and commercially awkward.
Prequalifying the fabricator: evidence, not sales material
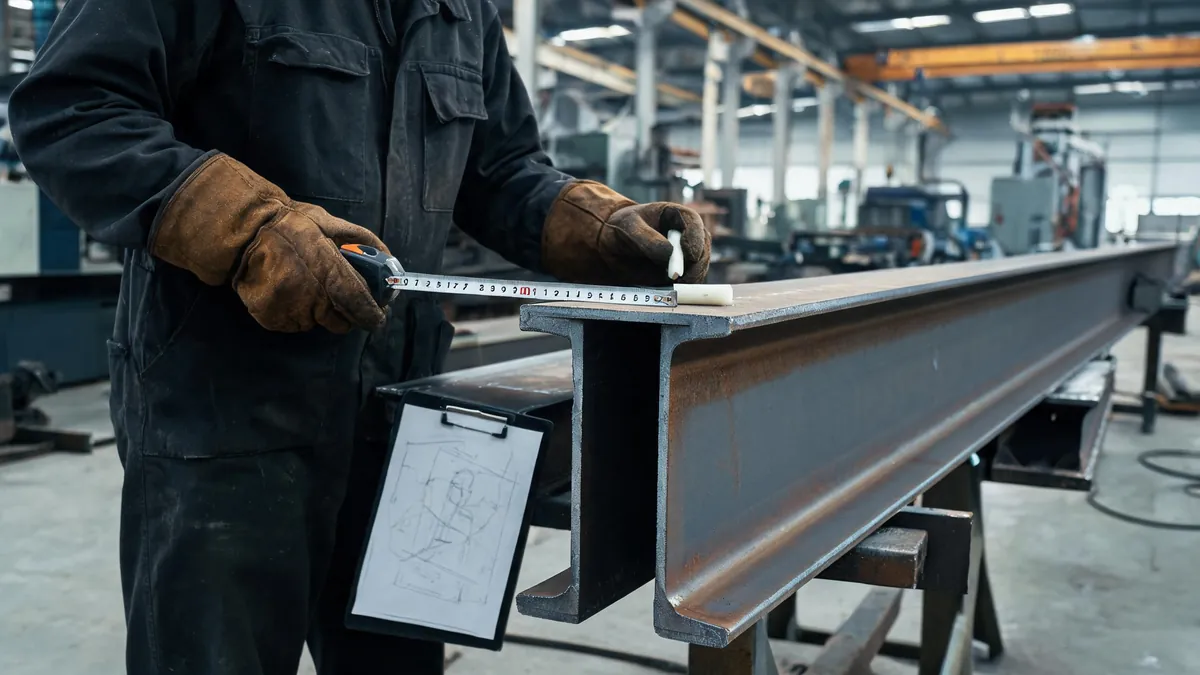
Any supplier can send a capability brochure. What you want is the evidence trail behind the framing you are buying. For a warehouse package with hot rolled primary members, ask for:
- Factory production control certificate under a recognised execution standard (for example EN 1090 execution class 2 or 3, or an equivalent national scheme), covering the classes relevant to your structure.
- Welding procedure specifications and qualification records, with the welder qualification list validity dates.
- NDT capability and scope: which methods are done in house, which are subcontracted, and what percentage of which joints is inspected.
- Dimensional inspection practice: who measures, with what, and what the report looks like.
- Material traceability procedure: how heat numbers are marked and recorded from receipt to packing.
- Coating control: in-house painting or blasting, galvanizing subcontractor, and how thickness is measured and recorded.
- Subcontracting policy: whether the primary members are actually fabricated on the site you are visiting.
Ask for a sample shipment file from a previous project — material certificates, dimensional report, NDT report, packing list. A fabricator with a functioning system can produce that file in a day. A trader cannot, which is exactly what the request is meant to reveal.
How specification choices move cost and lead time
| Decision | Steel cost | Fabrication cost | Lead time | Freight |
|---|---|---|---|---|
| Higher grade, lighter sections | Depends on rolling availability | Broadly unchanged | Rises if the size is not stocked | Falls slightly — less weight, same volume |
| Built-up welded rafters instead of rolled | Broadly unchanged per tonne | Rises clearly | Rises — cutting, fit-up, NDT | Broadly unchanged |
| Hot dip galvanizing added | Rises | Rises — venting, handling, straightening | Rises — third-party process queue | Broadly unchanged |
| Crane loading added | Rises | Rises — fatigue details, tighter tolerance | Rises | Rises with heavier members |
| Drawings approved late or revised after cutting | Rises through rework | Rises sharply | Rises sharply | Unchanged |
| Bolt and connection standardization | Falls slightly | Falls | Falls | Unchanged |
A seven-step specification sequence that avoids rework
- Fix the design basis: span, bay spacing, eave height, roof and wall build-up, crane and floor loads, wind and snow data, service temperature.
- Select the structural system and the primary member family.
- Select grades against the design code and the toughness requirement, and check local availability with the fabricator before locking the material list.
- Define surfaces: preparation grade, protection system, treatment of cut edges and welds, holes for galvanizing drainage.
- Define connection philosophy: bolted on site where possible, welded in the shop, with splice and haunch positions on the drawings.
- Define the documentation and inspection package, including witness points and who pays for third-party inspection.
- Release for fabrication only after the drawing revision, the material list and the inspection plan are aligned and signed.
Common mistakes in hot rolled framing specification
- Buying on price per tonne alone. Scope differences hide inside that number; compare the scope table, then the rate.
- Accepting a certificate without a traceability link. A mill certificate for the heat is not evidence that your members came from that heat unless the marking scheme connects them.
- Treating grades as freely interchangeable. Strength may match, toughness and weldability may not.
- Leaving cut edges and welds out of the coating specification. They corrode first and are visible during handover.
- Specifying galvanizing without vent and drain details. Trapped liquid and distortion are expensive to fix after fabrication.
- Approving drawings late and then asking for the original delivery date. Fabrication is a queue; late approval moves the whole chain.
- Never visiting or verifying the production site. If the primary members are subcontracted, the quality system you audited is not the one building your frame.
Frequently asked questions about hot rolled steel framing
Is hot rolled steel framing stronger than cold formed framing?
Not in absolute terms — the two are engineered differently. Hot rolled sections are thicker-walled and carry heavy concentrated loads and longer spans more naturally, which is why they dominate primary frames in warehouses and industrial buildings. Cold formed sections are efficient in thin-walled, repetitive elements such as purlins and girts. Strength comes from the design, not from the forming method; what changes is where each system is economical.
How do I verify that the steel delivered is the grade I specified?
Three checks together: the mill test certificate for the heat number, the fabricator’s material record linking that heat to your member marks, and a physical check that the member marks match the packing list and the shop drawings. If you have a third-party inspector, define a marking check before the material is cut — after cutting, traceability is much harder to reconstruct.
Can we reduce cost by using a thinner section of a higher grade?
Sometimes, but deflection and vibration usually govern before strength does in long span frames. A lighter, higher-strength section may satisfy the strength check and still be rejected on deflection limits or on serviceability criteria agreed with the end user. Ask your designer to report both, and check that the section is actually rolled and available in the size you need.
What must be in the purchase order for hot rolled framing?
Section list with grades, drawing revision reference, preparation and coating specification, inspection and witness point list, documentation package, marking and traceability requirement, packing and shipping terms, and the substitution procedure. Anything you intend to enforce should appear there, because a shop-floor discussion at the end of fabrication rarely produces a good outcome.
How long does fabrication take after drawings are approved?
It depends on tonnage, complexity, section availability and the coating process. A straightforward portal frame package and one with heavy crane beams, built-up rafters and galvanizing sit in completely different queues. Ask for a production schedule broken down by material purchase, cutting, welding, coating and packing, with the assumptions written down — that is far more useful than a single number of weeks.
Getting a specification review before you order
Send us your drawings, design basis and the section list you were quoted. We will review the primary member selection, the grade and toughness requirement, the connection and splice proposal, and the coating specification, and tell you where the package is likely to need clarification before fabrication starts. That review happens before cutting, which is the only point where it is cheap.
For a full picture of how the frame fits into the rest of the building — cladding, insulation, doors, ventilation and site work — start from our prefab steel warehouse systems page, and use the quality control guide to align the inspection points with your own project requirements. When you are ready to price the package, submit the design basis through our quotation form and we will come back with the section list, tonnage summary and documentation scope in writing.